Decision in one sentence: Accept a fast connector only when the exact connector model, preparation dimensions, cleave, assembly sequence, end-face condition, optical result, and technician record meet the approved work instruction. Visual appearance alone is insufficient.
Fast connectors place precision fiber preparation in the field. Performance depends on compatible fiber, tools, cleanliness, cleave quality, insertion depth, internal index-matching condition, strain relief, and consistent inspection.
This guide is written for FTTH field supervisors, installers, ISP quality teams, contractors, distributors, and connector buyers. It focuses on the project decisions that belong in drawings, work instructions, samples, test records, and purchase orders. It does not invent a DIMI-specific rating, certification, or performance value. Any model-specific limit must be confirmed from the current product page, approved drawing, data sheet, or authoritative project source.
For the broader product family, review fiber optic connectors and the DIMI product portfolio.
Acceptance Summary
The following matrix keeps the purchase decision tied to observable evidence rather than a short product label.
| Decision factor | Question to answer | Evidence to request | Risk if missed |
|---|---|---|---|
| Connector-specific preparation | Are strip length, cleave length, and insertion method taken from the exact connector instruction? | approved model instruction, gauge, training sample, and observed installation | Using remembered dimensions from another connector model |
| Fiber and cleave quality | Is the fiber clean, undamaged, and cleaved correctly? | microscope or cleave inspection where available, cleaver condition, and reject criteria | High loss, unstable contact, or broken fiber inside the connector |
| Assembly confirmation | How does the installer confirm full insertion, lock, and strain relief? | connector indicators, pull/retention check allowed by instruction, and visual checkpoints | Fiber stops short, backs out, or carries cable tension |
| Optical acceptance | What measurement proves the installed connector is fit for service? | reference setup, wavelength, insertion-loss result, link budget, and retest rule | A link lights but has inadequate margin |
| Traceability and rework | Can failed work be linked to technician, tool, connector lot, and site condition? | label, work order, tool ID, lot, result, and rework record | Repeated failures cannot be traced to a common cause |
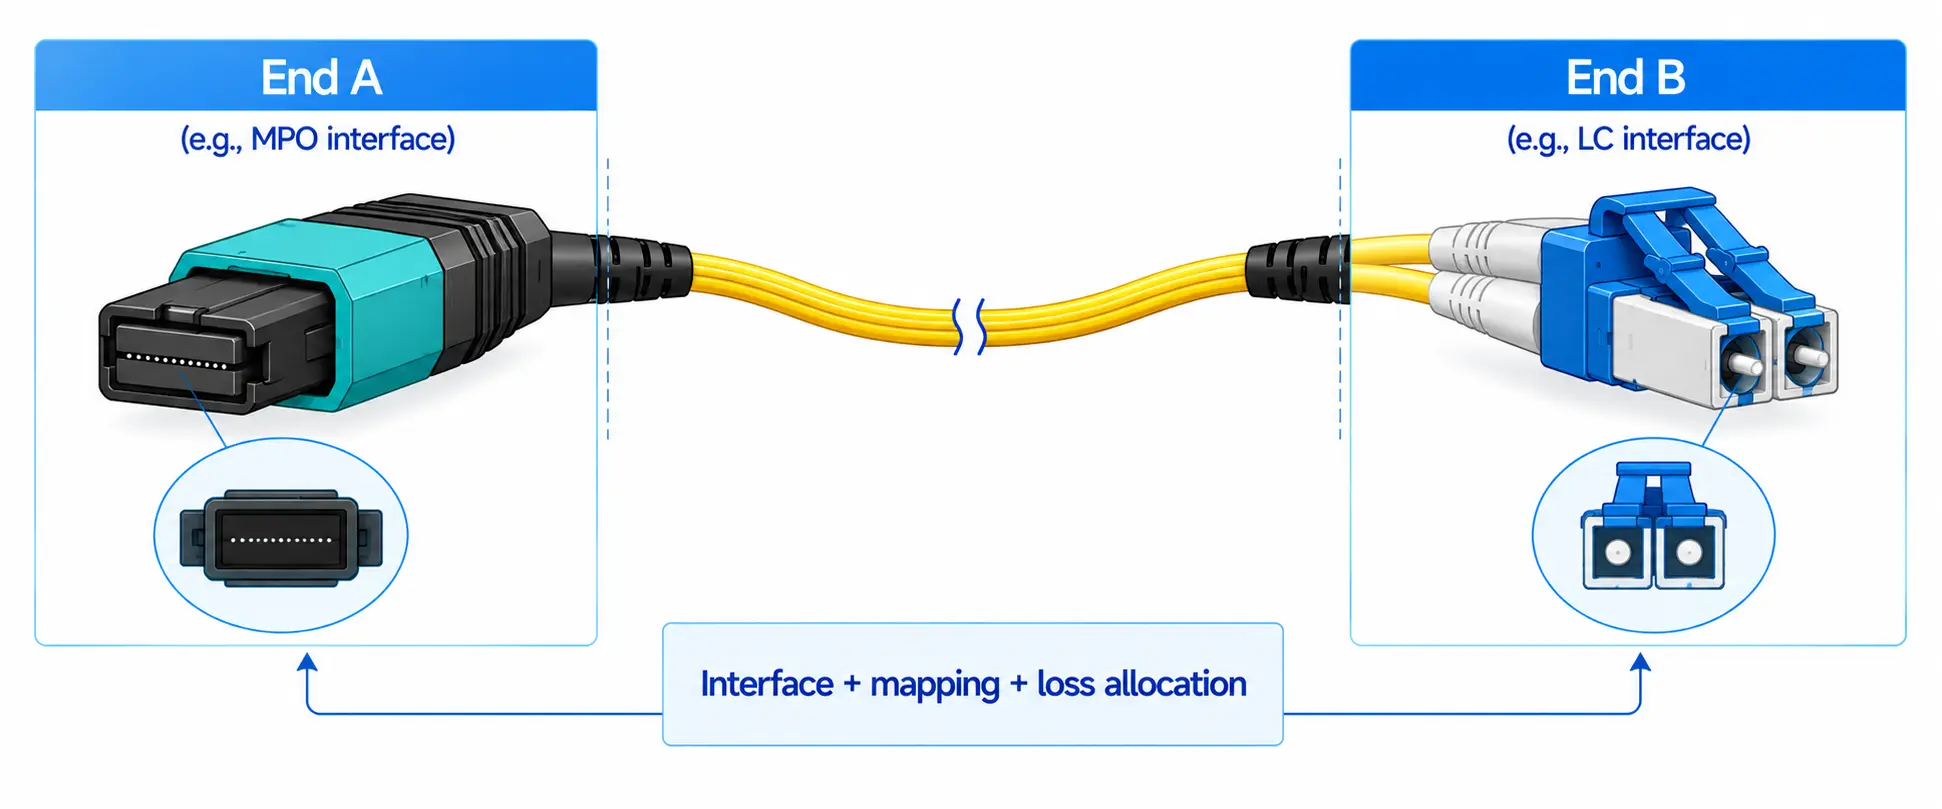
The practical rule is to compare complete configurations. Two items using the keyword sc fiber fast connector may differ in interface, construction, routing, test method, packaging, or change control. Price comparison is meaningful only after those fields are aligned.
Where Field Quality Is Won or Lost
Fast connectors place precision fiber preparation in the field. Performance depends on compatible fiber, tools, cleanliness, cleave quality, insertion depth, internal index-matching condition, strain relief, and consistent inspection. The component should therefore be treated as part of a controlled system rather than an isolated catalog item.
Start with the network or route drawing. Identify what connects on side A and side B, where load or optical power is transferred, which technician action occurs at the interface, and what remains accessible after the installation is complete. This prevents a common mistake: approving the part on a workbench while ignoring the enclosure, panel, pole, pathway, tool, or equipment that determines field performance.
Then separate three kinds of requirements. Functional requirements explain what the component must do. Interface requirements define what it must mate with or attach to. Evidence requirements define how the buyer will know that the delivered item matches the approved design. Keeping those categories separate makes substitutions and change requests easier to evaluate.
Use the DIMI cable assembly process as a reference for controlled assembly thinking, and review the fiber optic solutions page when the component belongs to a wider deployment.
Acceptance Factors That Change the Outcome
1. Connector-specific preparation
Decision question: Are strip length, cleave length, and insertion method taken from the exact connector instruction?
This factor changes the outcome because the part is installed inside a physical and operational boundary. A complete specification should name the relevant interfaces, construction, location, direction, and maintenance condition rather than relying on a family name. The engineering team should be able to point to a drawing or work instruction that shows how this field is used.
Evidence: Request approved model instruction, gauge, training sample, and observed installation. The evidence should identify the exact configuration and revision. A generic brochure may explain the product family, but it does not prove that the quoted assembly, module, closure, adapter, or hardware set matches the project.
Failure to prevent: Using remembered dimensions from another connector model. The corrective action is to issue model-specific work cards and prevent uncontrolled substitutions. Record the decision so that production, incoming inspection, installation, and maintenance use the same assumption.
2. Fiber and cleave quality
Decision question: Is the fiber clean, undamaged, and cleaved correctly?
This factor changes the outcome because the part is installed inside a physical and operational boundary. A complete specification should name the relevant interfaces, construction, location, direction, and maintenance condition rather than relying on a family name. The engineering team should be able to point to a drawing or work instruction that shows how this field is used.
Evidence: Request microscope or cleave inspection where available, cleaver condition, and reject criteria. The evidence should identify the exact configuration and revision. A generic brochure may explain the product family, but it does not prove that the quoted assembly, module, closure, adapter, or hardware set matches the project.
Failure to prevent: High loss, unstable contact, or broken fiber inside the connector. The corrective action is to maintain tools and reject visibly damaged preparation before insertion. Record the decision so that production, incoming inspection, installation, and maintenance use the same assumption.
3. Assembly confirmation
Decision question: How does the installer confirm full insertion, lock, and strain relief?
This factor changes the outcome because the part is installed inside a physical and operational boundary. A complete specification should name the relevant interfaces, construction, location, direction, and maintenance condition rather than relying on a family name. The engineering team should be able to point to a drawing or work instruction that shows how this field is used.
Evidence: Request connector indicators, pull/retention check allowed by instruction, and visual checkpoints. The evidence should identify the exact configuration and revision. A generic brochure may explain the product family, but it does not prove that the quoted assembly, module, closure, adapter, or hardware set matches the project.
Failure to prevent: Fiber stops short, backs out, or carries cable tension. The corrective action is to define observable hold points in the procedure. Record the decision so that production, incoming inspection, installation, and maintenance use the same assumption.
4. Optical acceptance
Decision question: What measurement proves the installed connector is fit for service?
This factor changes the outcome because the part is installed inside a physical and operational boundary. A complete specification should name the relevant interfaces, construction, location, direction, and maintenance condition rather than relying on a family name. The engineering team should be able to point to a drawing or work instruction that shows how this field is used.
Evidence: Request reference setup, wavelength, insertion-loss result, link budget, and retest rule. The evidence should identify the exact configuration and revision. A generic brochure may explain the product family, but it does not prove that the quoted assembly, module, closure, adapter, or hardware set matches the project.
Failure to prevent: A link lights but has inadequate margin. The corrective action is to use project-defined optical limits and preserve the measurement record. Record the decision so that production, incoming inspection, installation, and maintenance use the same assumption.
5. Traceability and rework
Decision question: Can failed work be linked to technician, tool, connector lot, and site condition?
This factor changes the outcome because the part is installed inside a physical and operational boundary. A complete specification should name the relevant interfaces, construction, location, direction, and maintenance condition rather than relying on a family name. The engineering team should be able to point to a drawing or work instruction that shows how this field is used.
Evidence: Request label, work order, tool ID, lot, result, and rework record. The evidence should identify the exact configuration and revision. A generic brochure may explain the product family, but it does not prove that the quoted assembly, module, closure, adapter, or hardware set matches the project.
Failure to prevent: Repeated failures cannot be traced to a common cause. The corrective action is to record enough data to identify training, tool, material, or environment trends. Record the decision so that production, incoming inspection, installation, and maintenance use the same assumption.
Six-Step Installation and Acceptance Workflow
- Survey the application. Focus on connector-specific preparation. Create a marked drawing with route, interfaces, access limits, and environmental conditions. Assign an owner and record unresolved assumptions before moving to the next gate.
- Translate the survey into specification fields. Focus on fiber and cleave quality. Write an end-A/end-B or route-position description with measurable construction and documentation requirements. Assign an owner and record unresolved assumptions before moving to the next gate.
- Compare complete configurations. Focus on assembly confirmation. Normalize supplier offers against the same fields and list every deviation or assumption. Assign an owner and record unresolved assumptions before moving to the next gate.
- Approve a production-intent sample. Focus on optical acceptance. Use the intended materials, labels, packaging, companion parts, and installation tools. Assign an owner and record unresolved assumptions before moving to the next gate.
- Validate installation and acceptance. Focus on traceability and rework. Run the real work sequence, inspect access and routing, and collect the planned optical or mechanical evidence. Assign an owner and record unresolved assumptions before moving to the next gate.
- Lock change control and records. Focus on connector-specific preparation. Freeze the drawing revision, part description, approved sample, test format, packaging, and notification rule. Assign an owner and record unresolved assumptions before moving to the next gate.
A sample is useful only when it represents production. Photograph the installed state, record part numbers and revisions, preserve test results, and list required corrections. A sample built with different materials or hand-selected components cannot control a later bulk order.
Installation and Integration Practices
Verify identity before installation: part number, revision, end designations, materials, labels, quantity, packaging, and the approved drawing. Segregate any item that cannot be traced to the approved configuration.
Protect optical end faces, sealing surfaces, cable jackets, and grip surfaces from contamination and damage. Keep caps and packaging in place until the work step requires removal. Do not place a part on dirty ground, a pole surface, or an unprotected bench and then treat later cleaning as equivalent to prevention.
Manage load and bend paths deliberately. Optical components need controlled routing; field hardware needs controlled transfer of mechanical load. In either case, the installed part should not force an adjacent cable, fiber, connector, seal, bracket, or enclosure into an unintended position.
Use model-specific instructions for cleave length, torque, tension, bend radius, heating, sealing, tool settings, or acceptance limits. This article intentionally avoids universal values where the exact construction and official instruction must control.
For related components, review fiber fast connectors and SC connectors. Where the work forms part of an FTTH route, the FTTH deployment guide can help place the component in the wider network.
Complete the work with photographs, labels, measurements or test results, tool and technician information, and an as-built update. Evidence gathered immediately is more reliable than a reconstruction after a failure.
Common Failure Modes and Corrective Actions
| Observed or potential problem | Probable specification gap | Verification | Corrective direction |
|---|---|---|---|
| Using remembered dimensions from another connector model | Connector-specific preparation not fully controlled | approved model instruction, gauge, training sample, and observed installation | Issue model-specific work cards and prevent uncontrolled substitutions. |
| High loss, unstable contact, or broken fiber inside the connector | Fiber and cleave quality not fully controlled | microscope or cleave inspection where available, cleaver condition, and reject criteria | Maintain tools and reject visibly damaged preparation before insertion. |
| Fiber stops short, backs out, or carries cable tension | Assembly confirmation not fully controlled | connector indicators, pull/retention check allowed by instruction, and visual checkpoints | Define observable hold points in the procedure. |
| A link lights but has inadequate margin | Optical acceptance not fully controlled | reference setup, wavelength, insertion-loss result, link budget, and retest rule | Use project-defined optical limits and preserve the measurement record. |
| Repeated failures cannot be traced to a common cause | Traceability and rework not fully controlled | label, work order, tool ID, lot, result, and rework record | Record enough data to identify training, tool, material, or environment trends. |
Before disturbing the installation, preserve the original state. Record photographs, labels, measurements, test data, part numbers, lot information, tool condition, weather or room conditions, and the work instruction used. A repair that erases the evidence may restore service but prevents root-cause learning.
If several failures share a lot, crew, cabinet, route, or tool, compare common inputs: drawing revision, material substitution, packaging, training, inspection method, tool wear, installation sequence, and the approved sample. Correct the system cause before replacing large quantities.
Procurement and Incoming-Acceptance Checklist
Place the following fields in one controlled RFQ, submittal, or purchase specification:
- Connector-specific preparation
- Fiber and cleave quality
- Assembly confirmation
- Optical acceptance
- Traceability and rework
- End-A and end-B interface or route position
- Finished dimensions and tolerance
- Materials and construction
- Labels and mapping
- Packaging and protection
- Required test or inspection record
- Lot or serial traceability
- Approved drawing and revision
- Sample approval status
- Change-notification rule
Ask suppliers the following questions before comparing price or lead time:
- How is connector-specific preparation defined for the quoted part, and which drawing, report, material document, or sample feature supports it?
- How is fiber and cleave quality defined for the quoted part, and which drawing, report, material document, or sample feature supports it?
- How is assembly confirmation defined for the quoted part, and which drawing, report, material document, or sample feature supports it?
- How is optical acceptance defined for the quoted part, and which drawing, report, material document, or sample feature supports it?
- How is traceability and rework defined for the quoted part, and which drawing, report, material document, or sample feature supports it?
- Will production be identical to the approved sample, and how will design or material changes be communicated?
- Which companion parts, tools, cleaners, seals, adapters, brackets, or replacement items are required but not included?
Send the application, quantity, drawings, interfaces, and required evidence through the DIMI project inquiry form. The DIMI Fiber team can clarify unresolved configuration questions before a reliable quotation is prepared.
Incoming inspection should verify identity, dimensions, construction, labels, packaging, visible condition, and representative function against the approved sample and drawing. Segregate unidentified or nonconforming material so it cannot be issued while the discrepancy is reviewed.
FAQ
Q: Is sc fiber fast connector a complete purchase specification?
A: No. It identifies a product or search family, but the buyer still needs to define interfaces, construction, dimensions, mapping, environment, evidence, packaging, and change control for the actual project.
Q: What should be verified before bulk production?
A: Verify system fit, mating or attachment interfaces, routing, installation sequence, maintenance access, labels, optical or mechanical acceptance, documentation, packaging, and traceability using the intended production construction.
Q: Can a supplier substitute a similar-looking configuration?
A: Only after the buyer evaluates the deviation against the controlled specification and approves it. Similar appearance or a shared catalog keyword does not establish functional equivalence.
Q: How should failed incoming material be handled?
A: Preserve evidence, identify the affected lot, segregate the material, compare it with the approved sample and drawing, and decide whether the issue is identity, construction, workmanship, packaging, documentation, or application mismatch.
Q: When is a sample approval not enough?
A: A sample is insufficient when production materials, tools, labels, packaging, or test methods can change without control. Pair sample approval with a revision-controlled drawing and a change-notification requirement.
Conclusion
Accept a fast connector only when the exact connector model, preparation dimensions, cleave, assembly sequence, end-face condition, optical result, and technician record meet the approved work instruction. Visual appearance alone is insufficient. The best decision is traceable from the application survey to the drawing, BOM, sample, work instruction, acceptance record, and maintenance plan.
DIMI Fiber supports project-based configuration across fiber assemblies, passive components, enclosures, connectors, and outdoor hardware. Use the project inquiry form for a configuration review, and verify all model-specific values against current approved product information before publication or purchase.