Preconnectorized and field-spliced FTTH distribution are not simply "fast" versus "low cost." They move work, risk, inventory, testing, and restoration to different points in the deployment process. The right choice depends on where you want optical joints to be made, how predictable the route is, what skills are available in the field, and how the network will be activated and repaired later.
This guide focuses on that deployment-model decision. For general enclosure sizing, ports, splice capacity, adapters, IP protection, and cable-entry selection, use the fiber termination box buying guide. For installation procedures after the architecture is fixed, see the FTTH termination box installation guide.
First, Define What "Preconnectorized" and "Spliced" Mean in Your Design
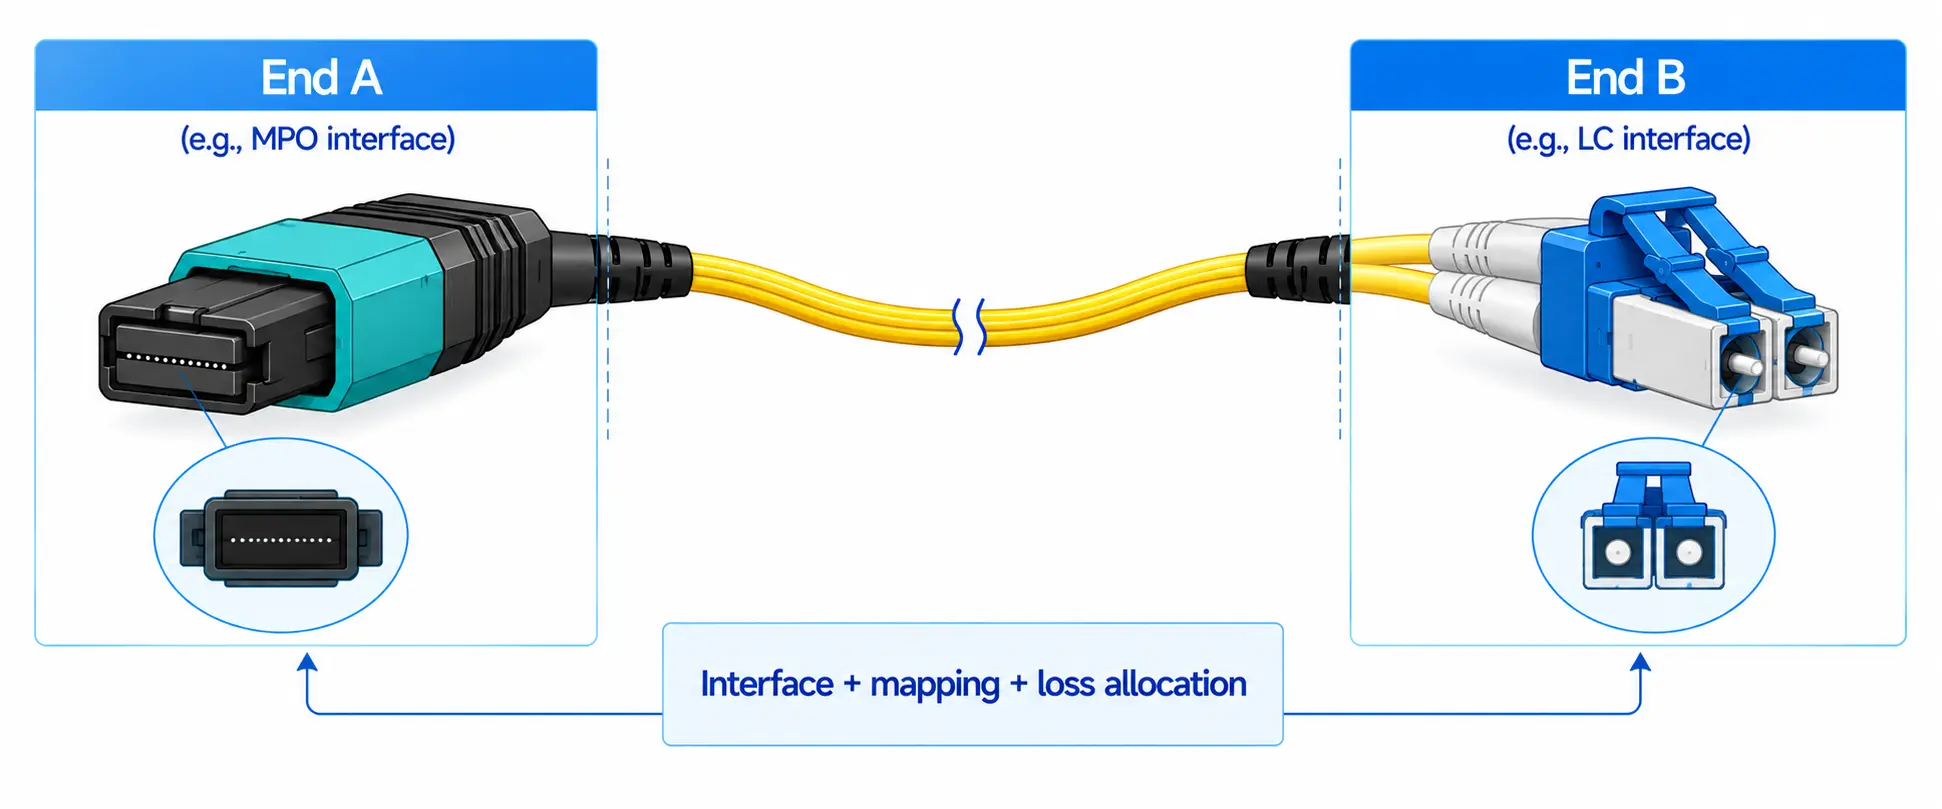
The labels are often used too loosely. A box can arrive with factory-installed adapters, pigtails, or a splitter and still require field fusion splicing on the feeder side. A terminal can also use hardened factory connectors for subscriber drops while its upstream cable is spliced at another location. Before comparing options, draw the actual optical path and mark where every removable connection and permanent splice will occur.
| Deployment model | Where most termination work happens | Typical field task | Main control point |
|---|---|---|---|
| Preconnectorized distribution | Factory-prepared cable assemblies, terminal ports, or pigtail/adapter assemblies | Route, inspect, clean, mate, label, and test approved connectors | Accurate route planning, interface compatibility, cleanliness, and cable/leg length |
| Field-spliced distribution | Fusion splicing and tray management at the deployment site | Prepare cable, splice fibers, protect splices, route slack, label, and test | Splicing skill, tools, cable preparation, tray capacity, and field quality control |
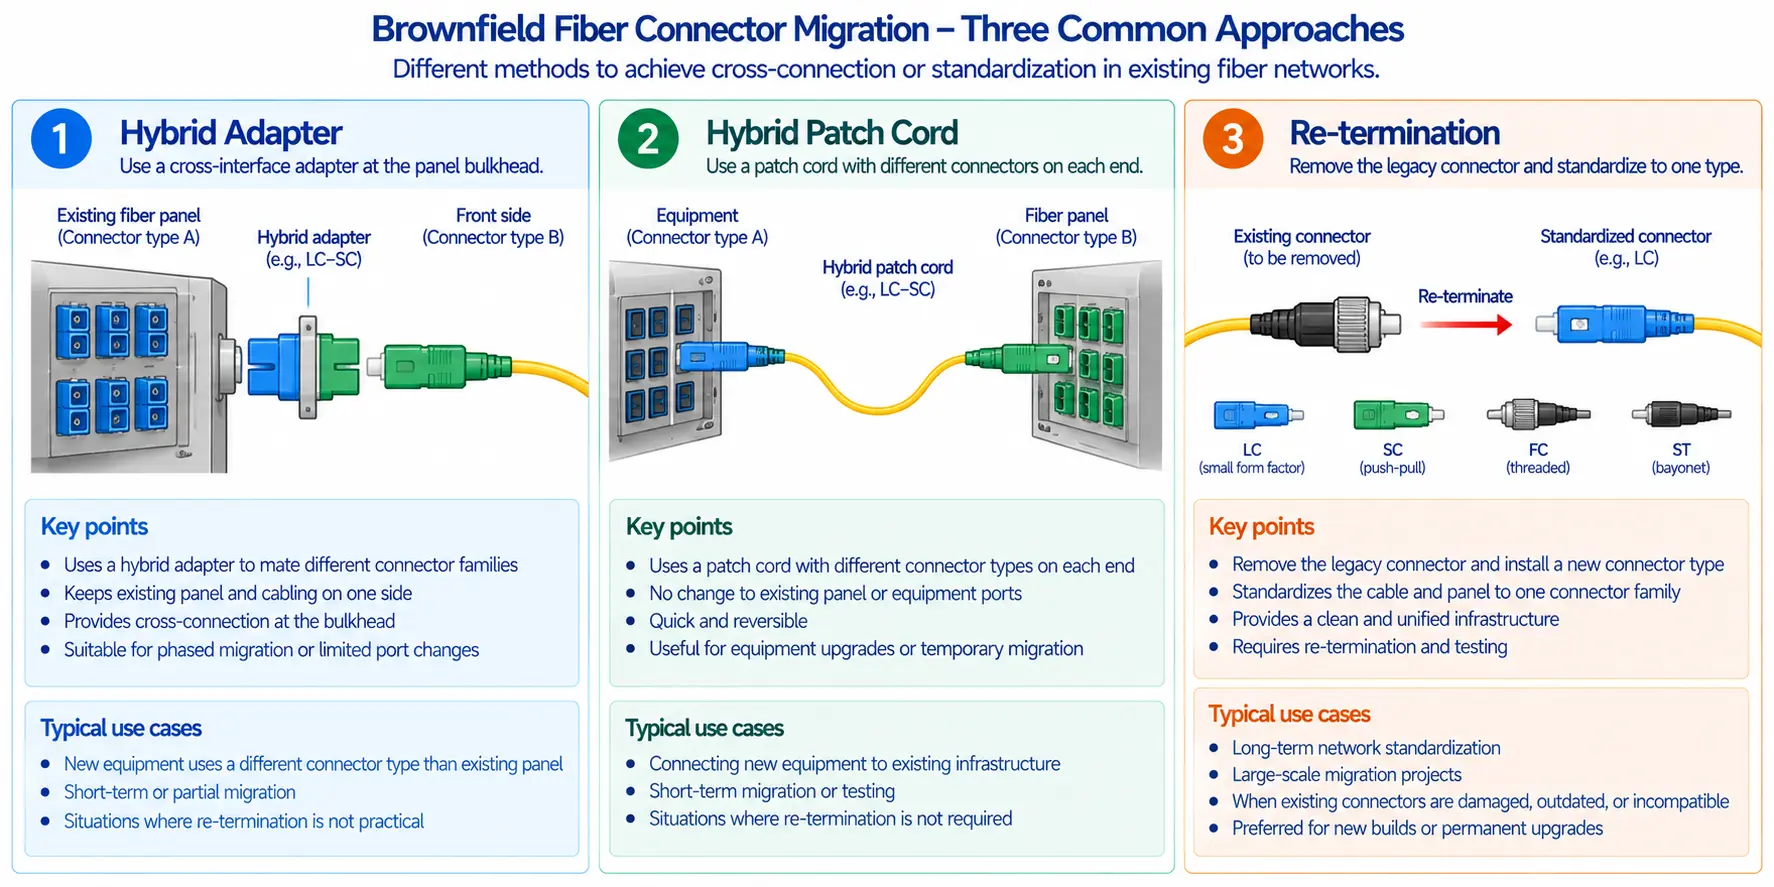
| Hybrid distribution | Split between factory and field | For example, splice the feeder into a terminal while using connectorized subscriber drops | A clear boundary between the spliced and connectorized portions of the network |
The Fiber Optic Association describes the same practical evolution in FTTH: prefabricated systems can remove much of the field splicing, while hybrid closures and terminals can combine splices with connectorized drop interfaces. Its FTTH network design reference is useful background when deciding where the factory/field boundary should sit.

The Core Decision: Where Do You Want Complexity to Live?
Preconnectorization does not remove engineering work; it moves more of it upstream. Field splicing does not remove inventory or testing; it gives the crew more freedom to adapt cable lengths and branch conditions at the site. The comparison is therefore a transfer of complexity rather than a universal technology ranking.
| Decision factor | Preconnectorized approach tends to favor | Spliced approach tends to favor |
|---|---|---|
| Route certainty | Well-surveyed routes, repeatable terminal locations, known cable or stub lengths | Routes where final length, entry direction, or branch position may change in the field |
| Field labor | Crews focused on placement, inspection, cleaning, mating, labeling, and testing | Crews with fusion-splicing equipment, cable-preparation tools, and splice-management skill |
| Activation model | Repeated subscriber adds through controlled connectorized interfaces | Planned construction windows where multiple fibers are spliced and commissioned together |
| Inventory model | Controlled connector types, cable lengths, port configurations, dust caps, and replacement assemblies | More flexible field cable lengths plus splice consumables, pigtails, trays, and splicing equipment |
| Restoration model | Replace or remate defined connectorized components when they are field-replaceable | Re-enter the box and resplice damaged fibers when the cable and tray design allow it |
| Design change tolerance | Best when the installed geometry is known before production | More tolerant of last-minute length and routing changes, within the approved enclosure and cable design |

Preconnectorized FTTH Requires Better Route Data Before Production
A factory-prepared assembly must be built to a defined configuration. That means route measurements, terminal locations, connector interfaces, cable entry direction, service loops, labels, and installation sequence need to be settled earlier than they would be in a field-cut-and-splice design.
The FOA notes that prefabricated cabling systems depend on knowing where the cable will be routed so lengths can be specified. This is the key trade-off: less termination work at the site requires stronger design control before the material is produced.
For each preconnectorized segment, document:
- from/to location and network function;
- exact connector family and polish at each mating point;
- cable type and installation environment;
- ordered length, permitted tolerance, and where excess length may be stored;
- entry direction and strain-relief method;
- port or branch identifiers;
- protective caps and connector-handling method;
- approved replacement strategy if a connector or factory lead is damaged.
A cable that is too short cannot be corrected by good installation technique. A cable that is excessively long can also create routing and slack-storage problems. Length control is therefore a design input, not a packaging detail.
Field-Spliced FTTH Moves More Quality Control to the Site
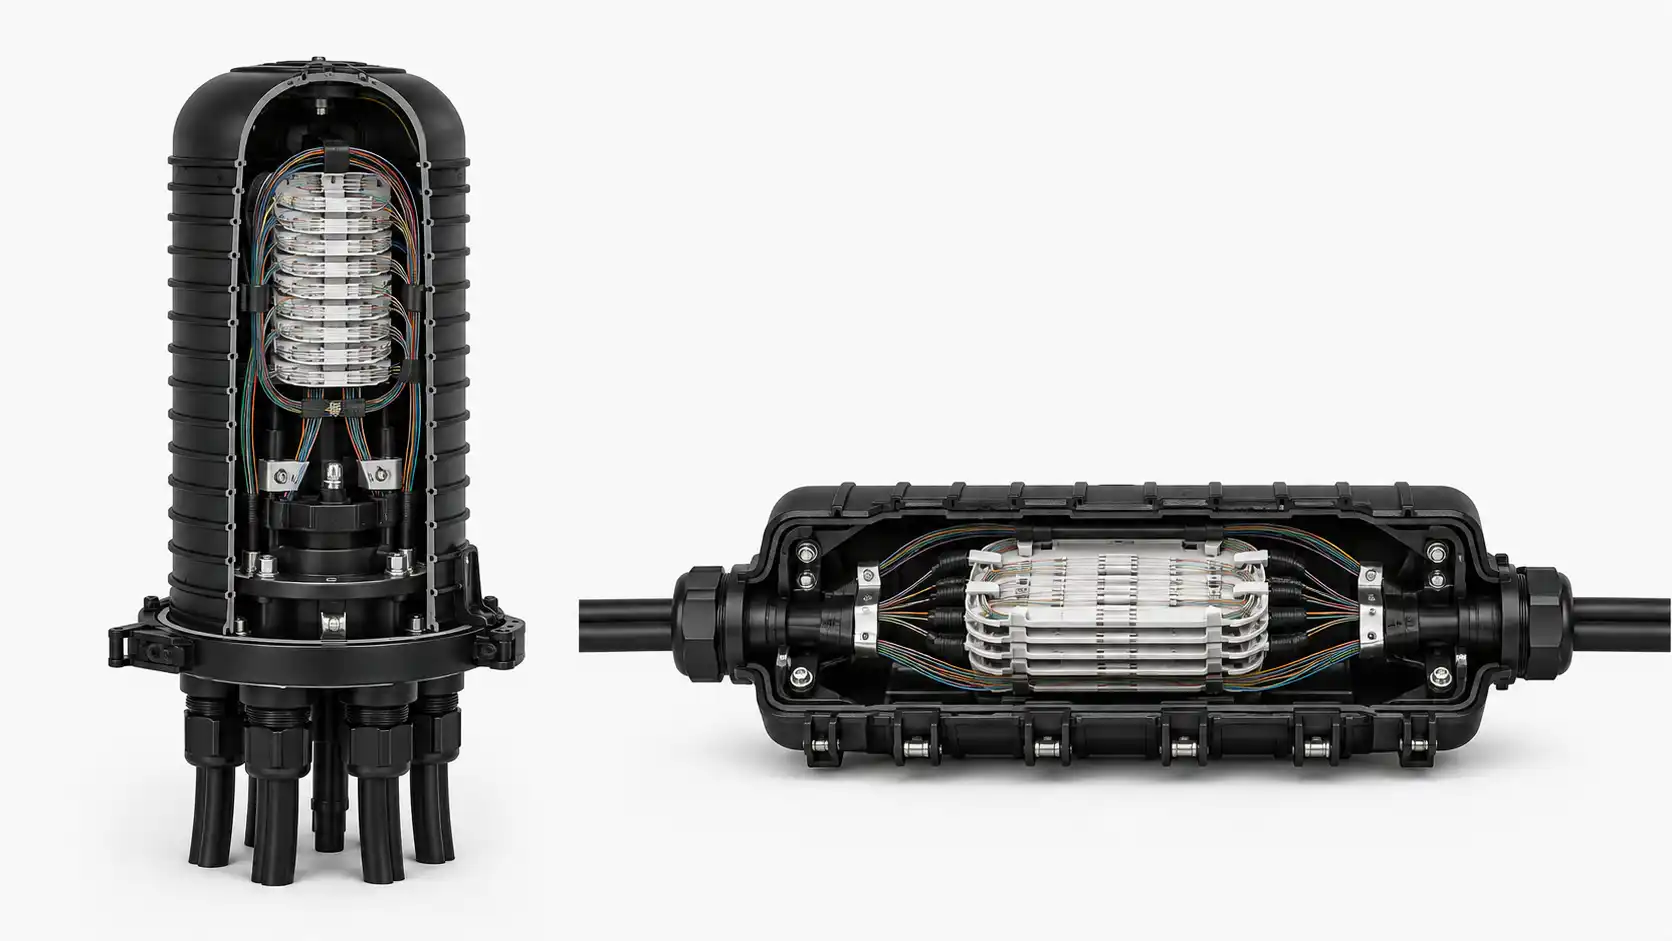
A spliced architecture allows the installer to cut and prepare cable for the actual route, but the site becomes the production environment for the optical joint. The box must provide enough access, cable anchoring, tray space, routing space, and slack management for the specified splice count and cable construction.
The field plan should define the complete splice process without inventing universal settings. Cleave preparation, fusion-splicer program, splice-protector type, stripping dimensions, tray loading, cable anchoring, bend limits, and acceptance criteria must follow the approved cable, box, equipment, and project instructions.
Spliced distribution is especially sensitive to operational readiness. Before deployment, verify that the project can consistently provide trained technicians, maintained tools as required by the operator, clean work practices, splice consumables, and a method to record fiber-to-port mapping.
Count Optical Events Across the Whole Link
Do not decide between the two architectures using a generic statement such as "splices are lower loss" or "factory connectors are low loss." The useful engineering question is how many optical events the complete path contains and what acceptance limit applies to the selected PON design.
Build a link diagram and count:
- fusion splices;
- mated connector pairs;
- splitter stages;
- patching or test access points;
- any additional transition introduced by repair or expansion.
Use verified component data and the project link budget for design values. After installation, test the finished optical path using the operator-approved method. The architecture should be accepted on the performance of the complete channel, not on one component's brochure value.

Subscriber Activation Can Change the Best Architecture
Construction and activation are different work events. A network may be built once but activate subscribers over months or years. If the distribution point will be revisited frequently for service turn-up, the access method at the drop side becomes an operational decision.
Connectorized drop interfaces can let a technician add service by inspecting, cleaning, mating, labeling, and testing an approved drop rather than opening a splice tray for every activation. A spliced drop architecture can still be appropriate when subscriber connections are installed in planned batches, when field splicing capability is readily available, or when the operator prefers permanent joints at that point in the network.
The FOA's FTTH installation reference describes both approaches and notes that re-enterable closures can use connectorized drops to support later additions. The practical lesson is to design around the real service workflow, not only the initial construction date.
Restoration and Spare Parts Belong in the Architecture Decision
A design is not complete until the maintenance team knows what can be replaced, what must be respliced, and which spares must be stocked.
For a preconnectorized design, ask:
- Can the damaged drop or lead be replaced independently?
- Are replacement lengths and connector interfaces standardized?
- Can a contaminated or damaged adapter be serviced without disturbing other active subscribers?
- Are protective caps, cleaning tools, and replacement assemblies part of the maintenance stock?
- What happens if a factory-integrated tail or internal harness is damaged?
For a spliced design, ask:
- Is sufficient service slack available for a future resplice?
- Can the target tray be accessed without disturbing unrelated fibers?
- Are splice protectors, pigtails, and cable-preparation consumables stocked?
- Can the repair crew identify the correct fiber and port from the as-built record?
- Is a fusion splicer available within the required restoration window?
This often leads to a hybrid architecture: permanent feeder or distribution fibers are spliced where route flexibility is valuable, while subscriber-facing interfaces are connectorized where repeated activation and replacement are expected.
Inventory: Fewer Field Operations Can Mean More Configuration Control
Preconnectorized systems can reduce field termination steps, but only if the correct assemblies reach the correct locations. The operator must control connector type, port count, cable/stub length, fiber assignment, labels, and mating compatibility. A visually similar assembly with a different length or interface can be unusable at the intended location.
Spliced architectures reduce dependence on pre-cut assembly length, but inventory still matters: cable type, pigtails, adapters, splice sleeves, trays, splitter configuration, glands or grommets, and repair consumables must match the approved design.
Compare the two models using SKU count, substitution risk, site-kitting effort, and restoration stock-not only unit price.

Acceptance Checklist: Test the Architecture You Actually Bought
| Acceptance item | Preconnectorized emphasis | Spliced emphasis |
|---|---|---|
| Identity | Assembly length, connector interface, labels, port mapping, revision | Cable type, pigtails/adapters, tray configuration, splice plan, revision |
| Physical installation | No connector strain; protected mating interfaces; controlled slack | Jacket and strength-member anchoring; protected splices; serviceable slack |
| Cleanliness | Inspect, clean if required, and re-inspect connector end faces before mating | Keep pigtail/connectors clean and protect prepared fibers and splice area |
| Mapping | Verify factory labels and port/fiber relationship | Verify field splice record and fiber-to-port relationship |
| Optical test | Test the completed channel against the project-approved acceptance limit and save the results with the as-built record | |
For either method, do not let a successful link-up replace formal acceptance. Preserve the box ID, route, cable/assembly IDs, splitter/port mapping, test records, photos, and any deviations from the approved drawing.
Common Failure Modes
| Problem | Likely design or process gap | Better control |
|---|---|---|
| Preconnectorized lead does not reach or leaves excessive slack | Route survey or length tolerance was not controlled | Freeze measured route and slack-storage location before production |
| Correct-looking connector cannot be used | Interface, polish, or mating format was not specified completely | Define both mating interfaces on the drawing and PO |
| Repeated dirty-connector faults during activation | Plug-and-play was treated as inspection-free | Include inspect/clean/re-inspect discipline in the activation procedure |
| Field splicing becomes the rollout bottleneck | Crew skill, splicer availability, or work-site conditions were not assessed | Validate labor capacity before choosing the field-spliced model |
| Repair affects unrelated subscribers | Restoration boundary and internal access were not planned | Define replaceable/spliceable units and service sequence before deployment |
| Quotes are impossible to compare | Suppliers assumed different termination architectures | Issue the same route, interface, test, documentation, and spare-part requirements to every bidder |
What to Put in an FTTH Distribution Box RFQ
When comparing an FTTH distribution box supplier, keep the commercial quote tied to the approved deployment model. Manufacturer or supplier wording should not replace the technical configuration.
- deployment model: preconnectorized, field-spliced, or hybrid;
- network location and box function;
- feeder/distribution/drop cable types and actual cable OD where relevant;
- port count, splice count, splitter requirement, and future reserve;
- connector type and polish for every removable optical interface;
- pre-installed pigtails, adapters, splitters, hardened ports, or cable stubs if required;
- ordered cable/stub lengths and tolerances;
- cable-entry, anchoring, and strain-relief requirements;
- labeling and fiber/port map format;
- factory and field acceptance records required by the project;
- replacement assemblies, consumables, and spare strategy;
- drawing revision and change-notification requirement.
For available commercial configurations, use the DIMI fiber distribution box category. This article should remain the deployment-architecture decision resource rather than the product-category owner.
Final Decision Rule
Choose preconnectorized, spliced, or hybrid FTTH distribution by deciding where you want precision work to happen and how the network will be maintained. If route geometry and interfaces can be frozen early, factory-prepared connectivity can reduce field termination steps. If field conditions change frequently and skilled splicing is readily available, a spliced architecture can preserve routing flexibility. In many deployments, the best answer is a controlled mix: splice where route adaptability matters, and use connectorized interfaces where repeated service activation and replacement matter.
FAQ
Q: Is a preconnectorized FTTH distribution box always faster to deploy?
A: It can reduce field termination work when the route, lengths, interfaces, and kitting are controlled. If the site geometry is uncertain or the wrong assembly arrives, the time advantage can disappear. Compare total planning plus field work, not only the connection step.
Q: Does a spliced FTTH box always have lower optical loss?
A: Do not assume a universal result. Count every splice, connector pair, splitter, and transition in the actual path, use verified component data for the design budget, and test the completed channel against the project limit.
Q: Is a loaded distribution box the same as a preconnectorized architecture?
A: No. A loaded box may contain adapters, pigtails, or a splitter but still require field splicing on one or more cable sides. Define the full optical path and where each termination is made.
Q: Can a network mix preconnectorized and spliced sections?
A: Yes. Hybrid designs are common because the feeder, distribution, and subscriber-drop segments can have different labor, routing, and maintenance requirements. The important control is a clear interface between the two methods.
Q: Which option is better for future subscriber adds?
A: It depends on the operating model. Connectorized drop interfaces can support later activation without creating a new splice at every add, while spliced architectures can work well when additions are handled by trained splice crews. Plan the service process and spare parts before choosing.